Launch of low-odor / low-fume cleaning & conditioning rubber series
PRECISION STARTS WITH A CLEAN MOLD
Cleaner molds.
Consistent production.
Cleaning and conditioning rubber sheets for semiconductor molding. Remove mold residues and prepare for the next production cycle.
ISO 9001:2015QUALITY MANAGEMENT
RoHS / SGSTESTED MATERIALS
CUSTOM COMPOUNDSMADE FOR YOUR PROCESS
INTEGRATED CIRCUITSDIODESTRANSISTORSLED & OPTO DEVICES
01 / ABOUT HANSCHEM
Rubber expertise.
Semiconductor focus.
HANSCHEM manufactures mold cleaning and conditioning rubber compounds for semiconductor packaging. We manage compounding, kneading, sheet forming, cutting and packing in-house. Product selection and custom dimensions are available to suit your process conditions.
Start of exports to China and Southeast Asia
Quality stability for storage at room temperature (≤25 °C); process-optimized compound design
ISO 9001:2015 Quality Management System certified
01CompoundingRaw materials
weighed & mixed
weighed & mixed
02KneadingUniform dispersion
in kneader mixer
in kneader mixer
03Roll MillingSheet forming
on roll mill
on roll mill
04CuttingCut to customer
dimensions
dimensions
05PackingPolyethylene zip bag
Moisture-resistant box
Moisture-resistant box
Packing & storage
Polyethylene zip bag / 10 kg net · Moisture-resistant coated carton
6 months at ≤25 °C · 12 months at ≤5 °C (from manufacturing date)
02 / QUALITY & CERTIFICATION
Quality you can verify.
Documentation you can access.
From our quality management system to product test reports, get the documentation your process review needs.
ISO 9001:2015
Quality management system
Certified in 2026 · IGC
RoHS / SGS
Conforms to RoHS · SGS test results
Heavy metals & PBBs/PBDEs: N.D.
MSDS
Safety data sheets for all products
Available on request
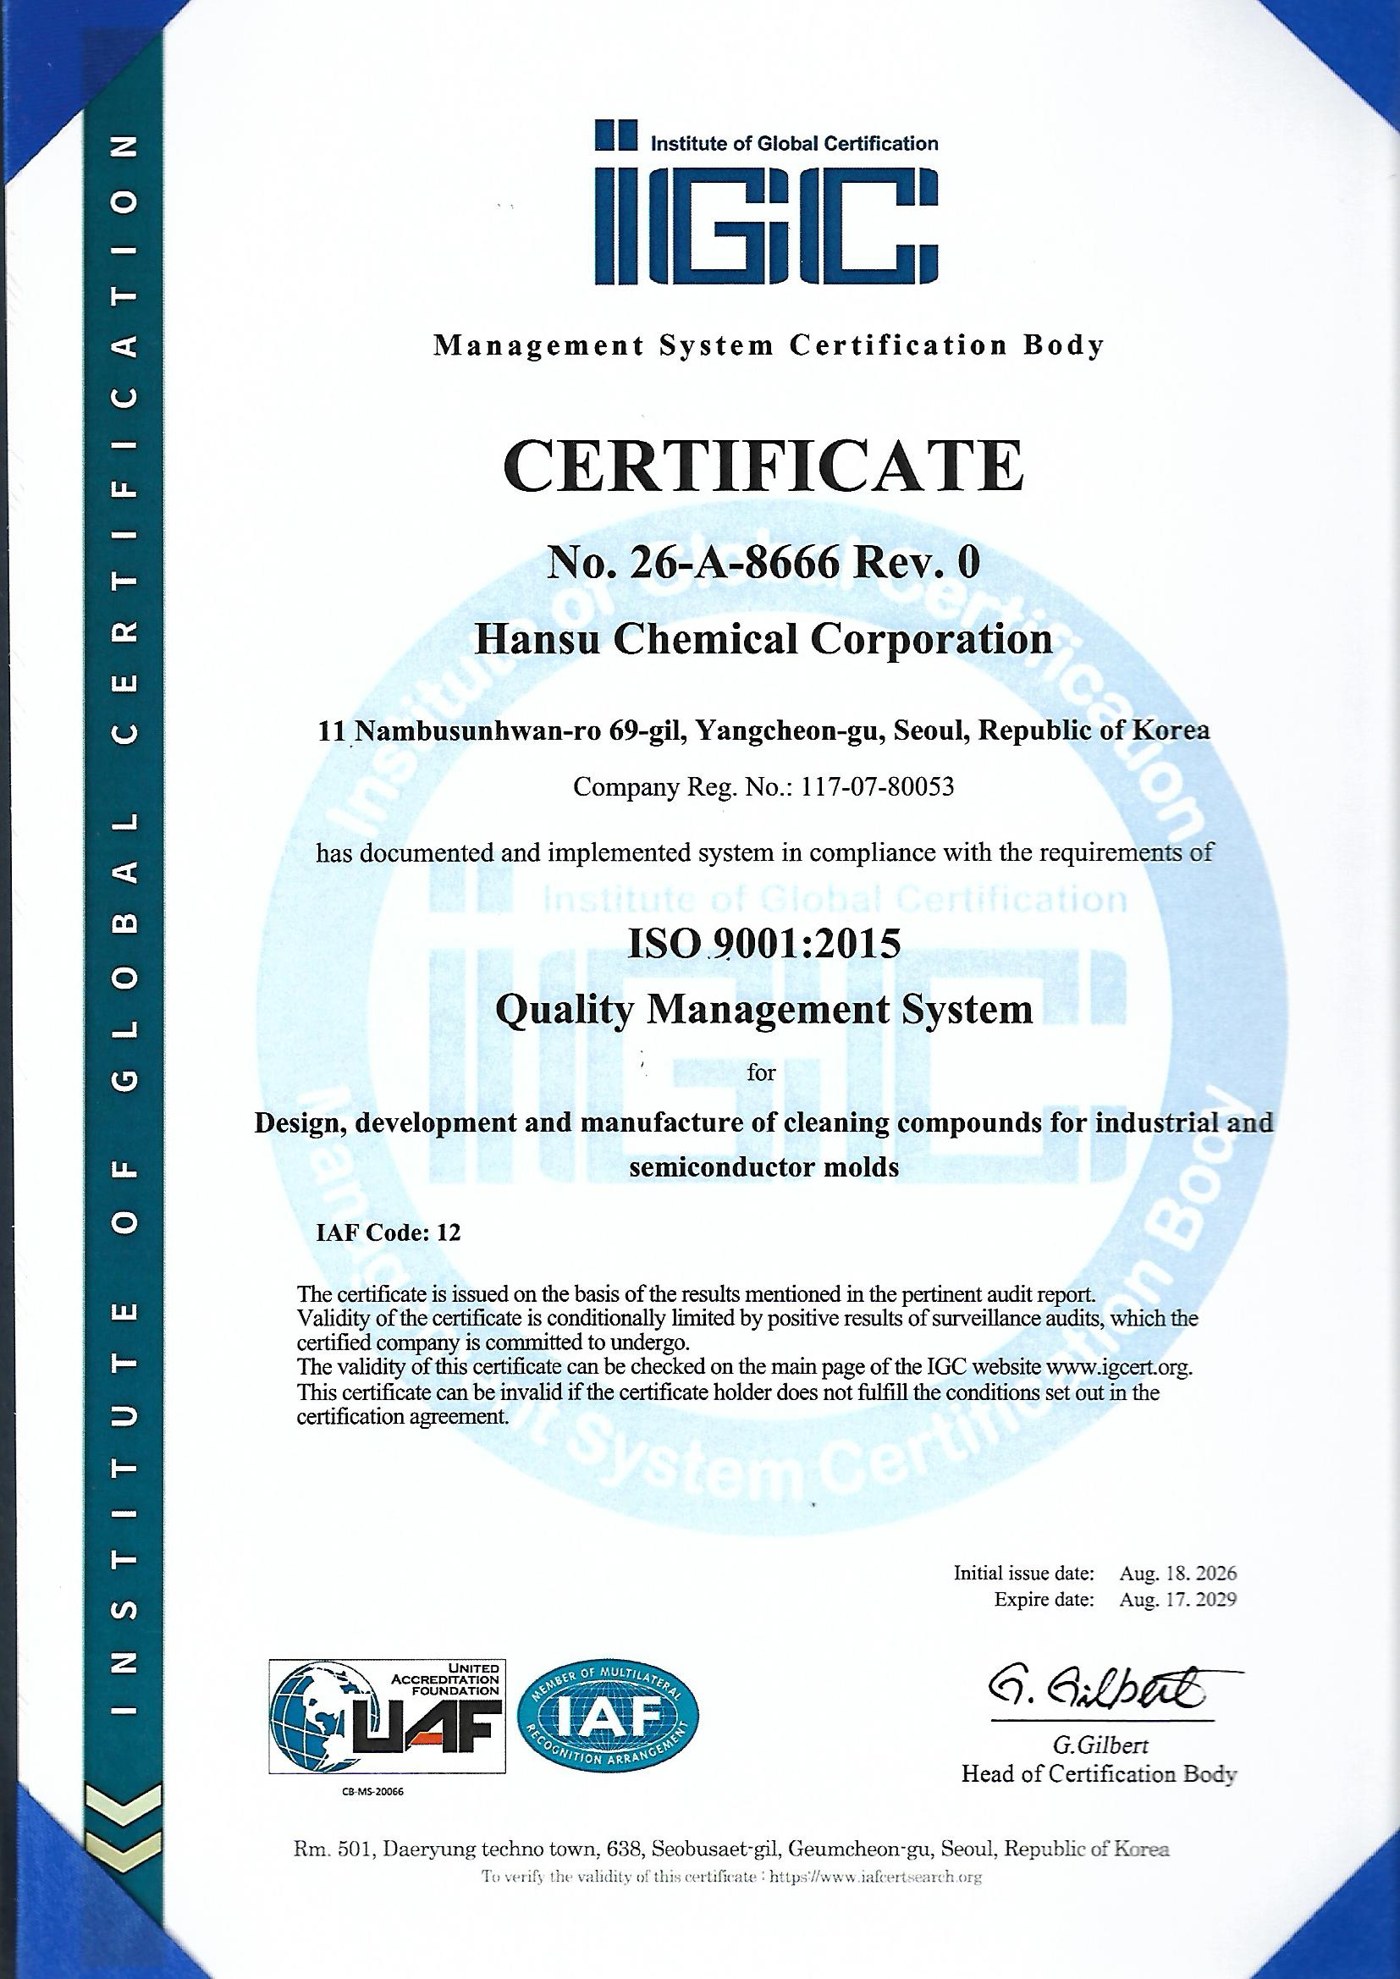
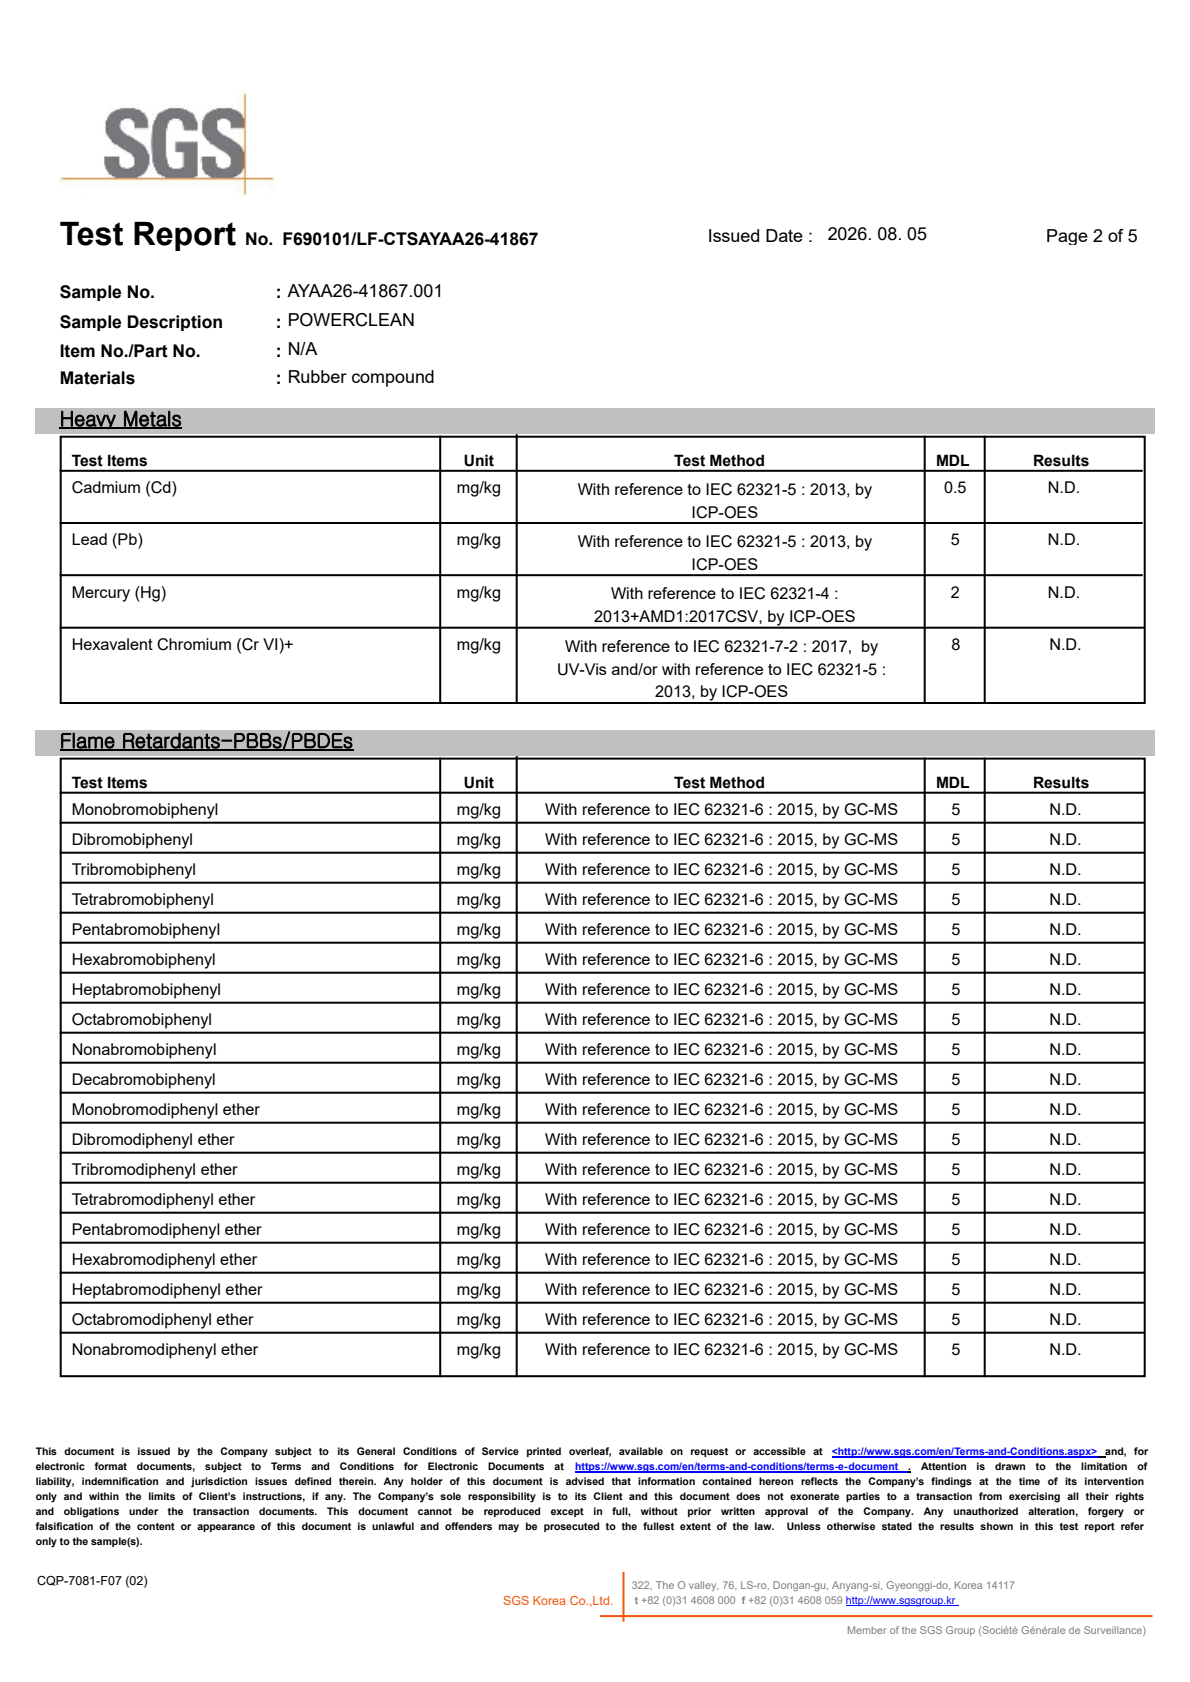
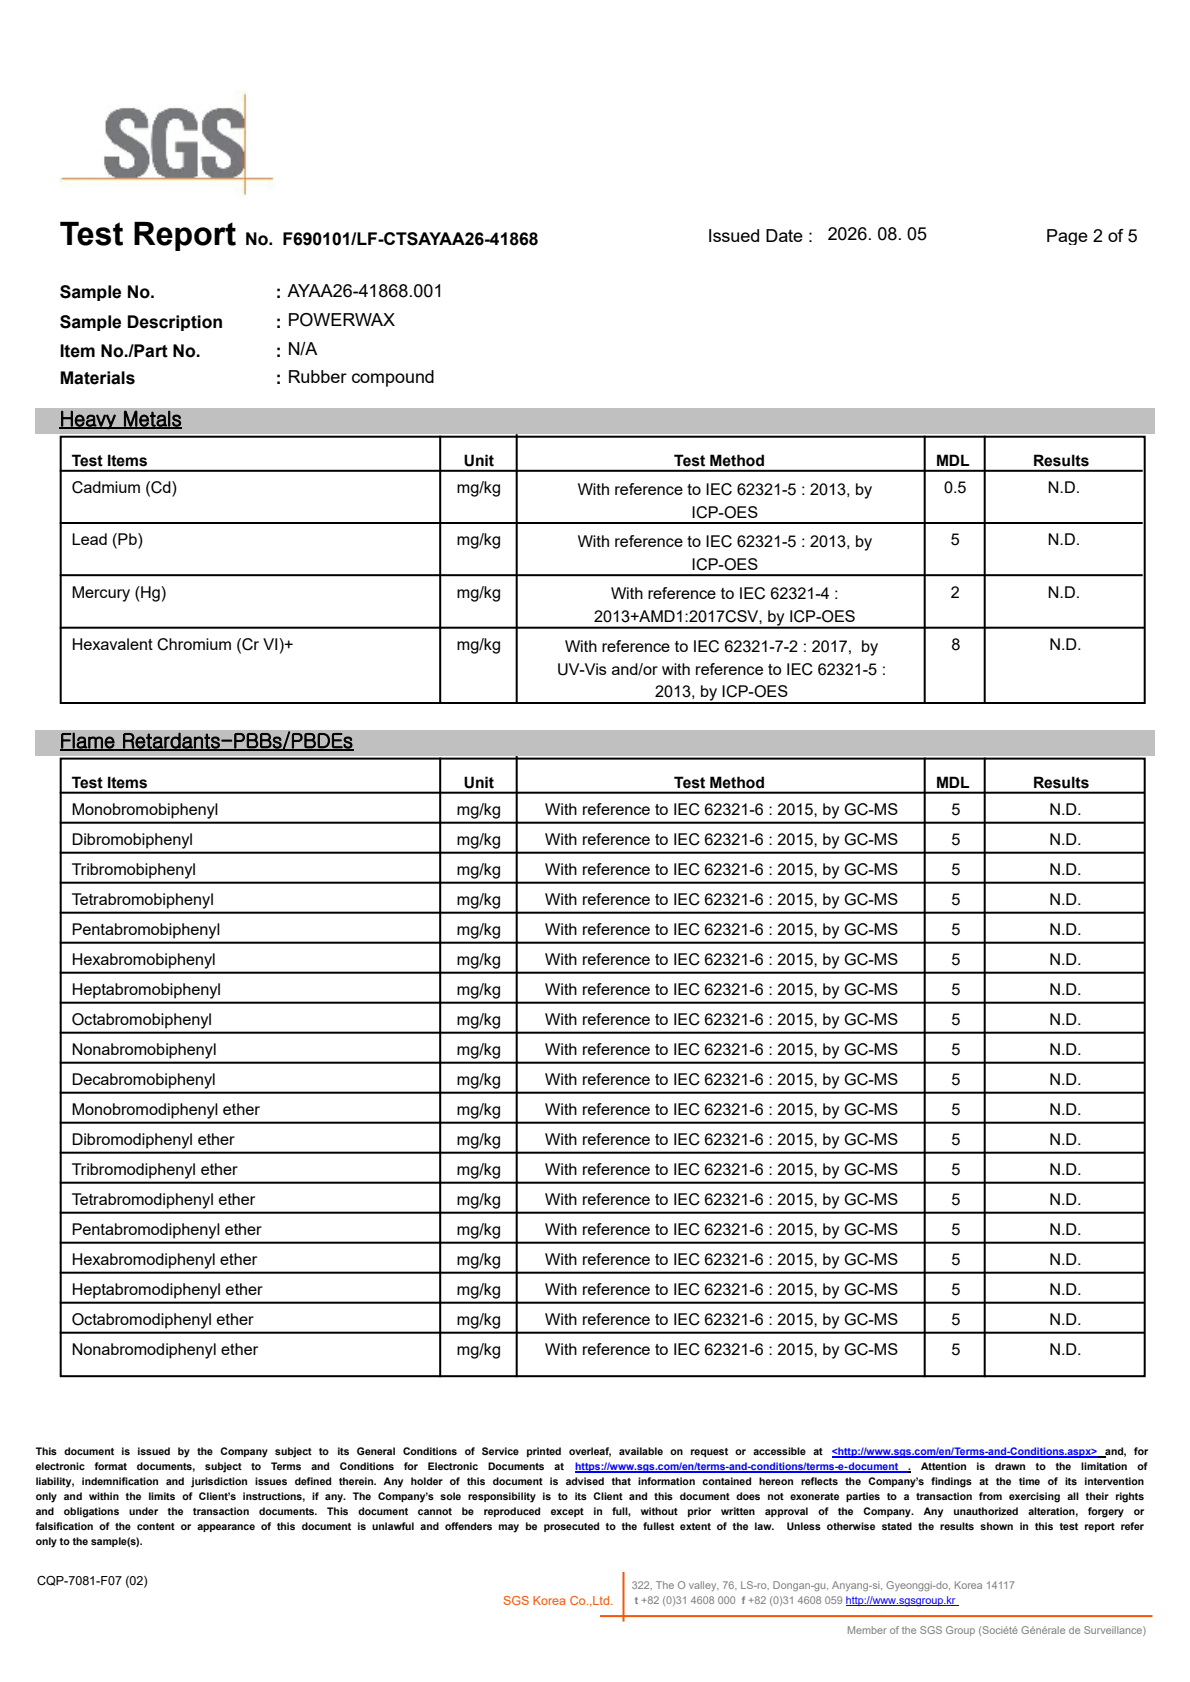
The ISO 9001 certificate, full SGS RoHS test reports (5 pages each) and product MSDS are available on request.
Request documents03 / OUR PRODUCTS
From cleaning to conditioning.
Two compounds. One workflow.
POWERCLEAN removes mold residues. POWERWAX restores release performance. Find the compound that fits your molding process.
01 / CLEANING COMPOUND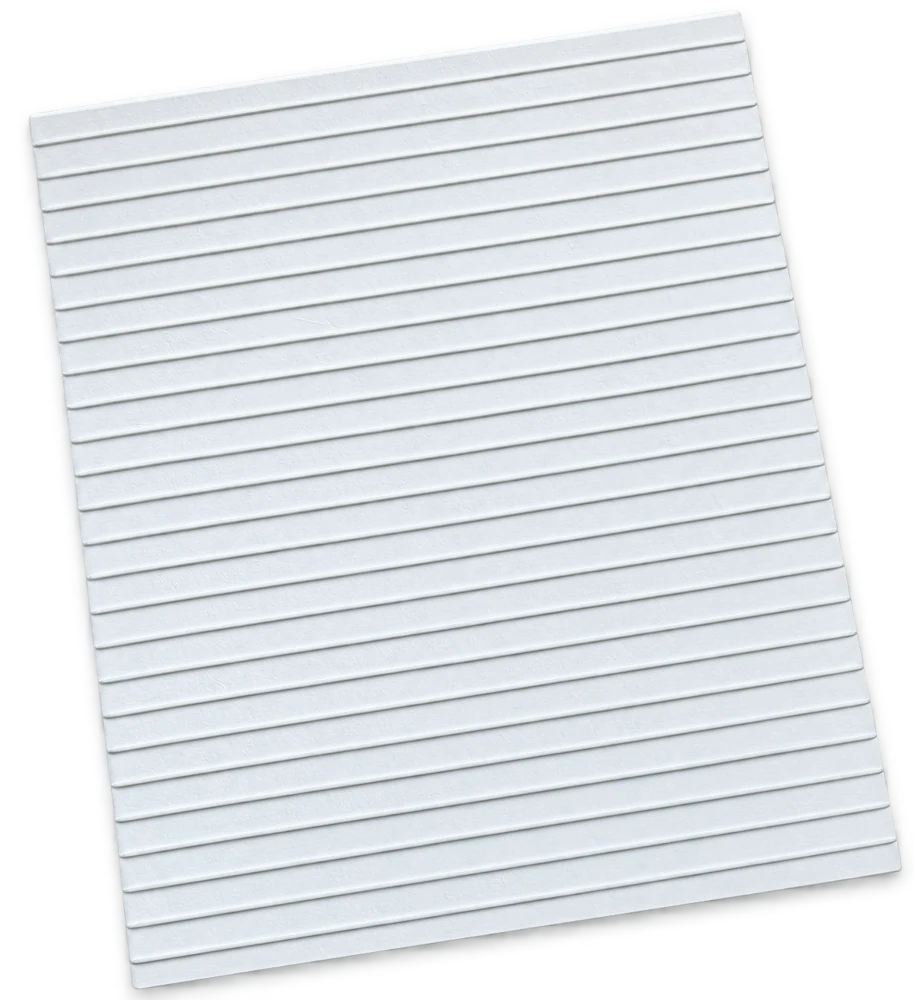 ENGINEERED FOR EMC MOLDING
MOLD CLEANING
Inquire about this product
POWERCLEAN
POWERCLEAN is a mold cleaning rubber compound for the removal of mold stains generated during epoxy molding compound (EMC) encapsulation of semiconductors such as integrated circuits, diodes, transistors and LEDs.
- Removes mold stains from cavities
- Removes residues from air vents and mold die faces
- No dummy lead frame · no preheating required
- Less pungent odor than melamine during mold cleaning
Mold temperature160–190 °C
Cure time3–7 min
Properties & process conditions
| Form | — | White rubber sheet |
|---|---|---|
| Filler | — | Titanium dioxide, Silica |
| Specific gravity | g/cm³ | 1.15 ± 0.15 |
| Molded density | g/cm³ | 1.15 ± 0.15 |
| Mooney viscosity | ML 140 °C | 70 ± 20 |
| Thickness | mm | 5, 7, 8, 9 |
| Clamp pressure | 30–100 kgf/m² |
|---|---|
| Mold temperature | 160–190 °C |
| Cure time | 3–7 min |
| Number of shots | 2–4 shots |
Length 200–300 mm / Width 10, 15, 20 mm / Thickness 5–10 mm
Other sizes available on customer request.
Model line-up 4 MODELS
- PC-2500C
- General applications
- PC-3000N
- High cleaning performance
- PC-3500H
- Lower odor with good cleaning performance
- PC-2900A
- LED / opto devices — low-temperature cure
02 / CONDITIONING COMPOUND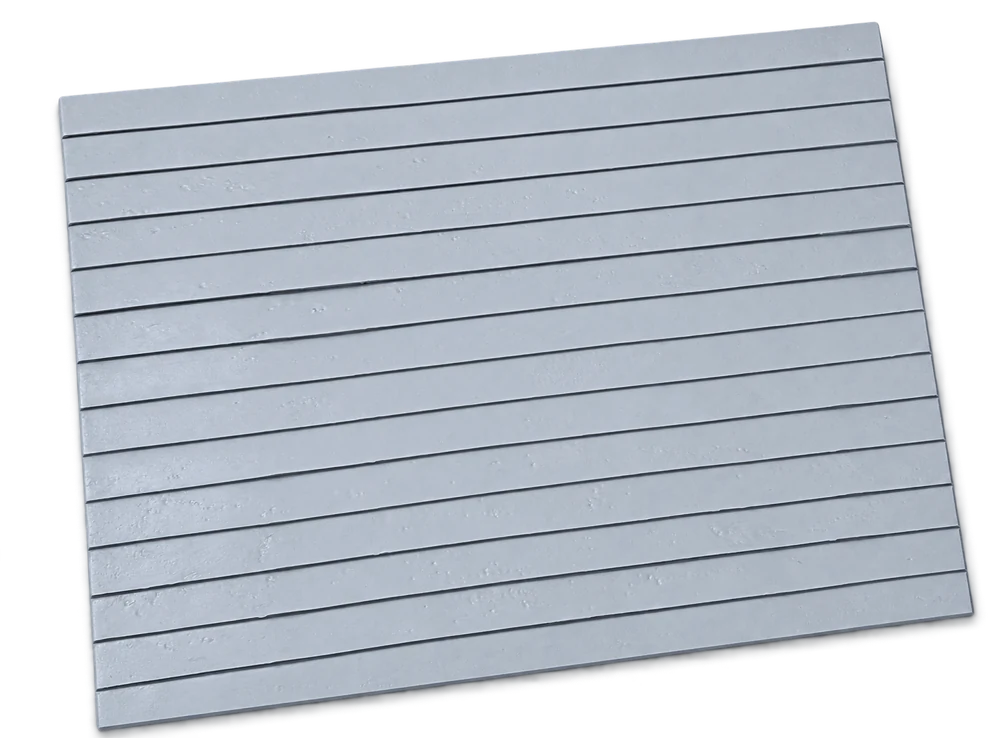 ENGINEERED FOR EMC MOLDING
MOLD CONDITIONING
Inquire about this product
POWERWAX
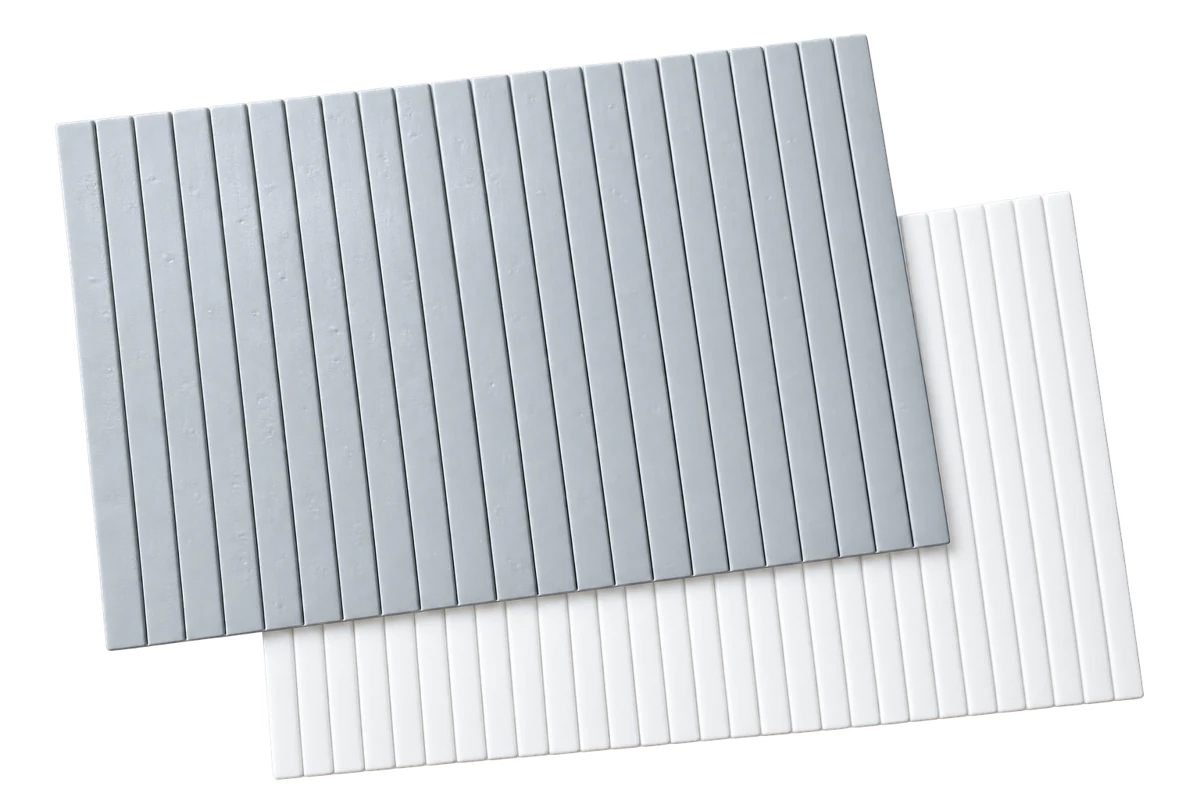
POWERWAX is a mold conditioning rubber compound applied to mold dies after the cleaning process in EMC encapsulation molding. It restores release performance and extends release life. Compression molding is recommended.
- Good release from mold after curing
- Conditions mold dies after curing
- No dummy lead frame · no preheating required
- 1–2 conditioning shots recommended
Mold temperature160–190 °C
Cure time3–5 min
Properties & process conditions
| Form | — | Gray rubber sheet |
|---|---|---|
| Rubber | — | EPDM |
| Specific gravity | g/cm³ | 1.15 ± 0.15 |
| Molded density | g/cm³ | 1.15 ± 0.15 |
| Mooney viscosity | ML 170 °C | 40 ± 20 |
| Thickness | mm | 5, 6, 7, 8, 9 |
| Clamp pressure | 30–100 kgf/m² |
|---|---|
| Mold temperature | 160–190 °C |
| Cure time | 3–5 min |
| Number of shots | 1–2 shots |
Length 200–300 mm / Width 10, 15, 20 mm / Thickness 5, 6, 7, 8, 9 mm
Other sizes available on customer request.
Model line-up 3 MODELS
- PW-4230C
- General mold conditioning
- PW-4500N
- High-efficiency conditioning compound
- PW-4700A
- LED mold manufacturing
04 / PROCESS PERFORMANCE
Cleaning & conditioning.
Shot comparison.
Compounds designed to reach sharp corners and air vents, then grip residues through expansion during cure.
165–180 °CMold temperature
180–300 sCuring time
2–3POWERCLEAN cleaning shots
| Item | Mold temp. | Curing time | Others (shots) | HANSCHEM |
|---|---|---|---|---|
| Cleaning · PC series | 165–180 °C | 180–300 sec | 4–5 | 2–3 |
| Conditioning · PW series | 165–180 °C | 180–300 sec | 2–3 | 1–2 |
Total cleaning + conditioning shots
Melamine
~9
Other rubber
5–7
HANSCHEM
3–5
CleaningConditioning
Fewer process steps
Reduced cleaning time — fewer shots, no lead frame step
Material information
RoHS test reports and MSDS available on request
Odor and fume
Designed to reduce odor and fume during cleaning
2–3 shots refers to POWERCLEAN cleaning alone. 3–5 total shots includes 2–3 cleaning shots and 1–2 POWERWAX conditioning shots.
Based on the HANSCHEM product catalog. Performance and operating conditions may vary by mold, residue and production environment.
05 / HOW IT WORKS
From mold inspection
to the next production run.
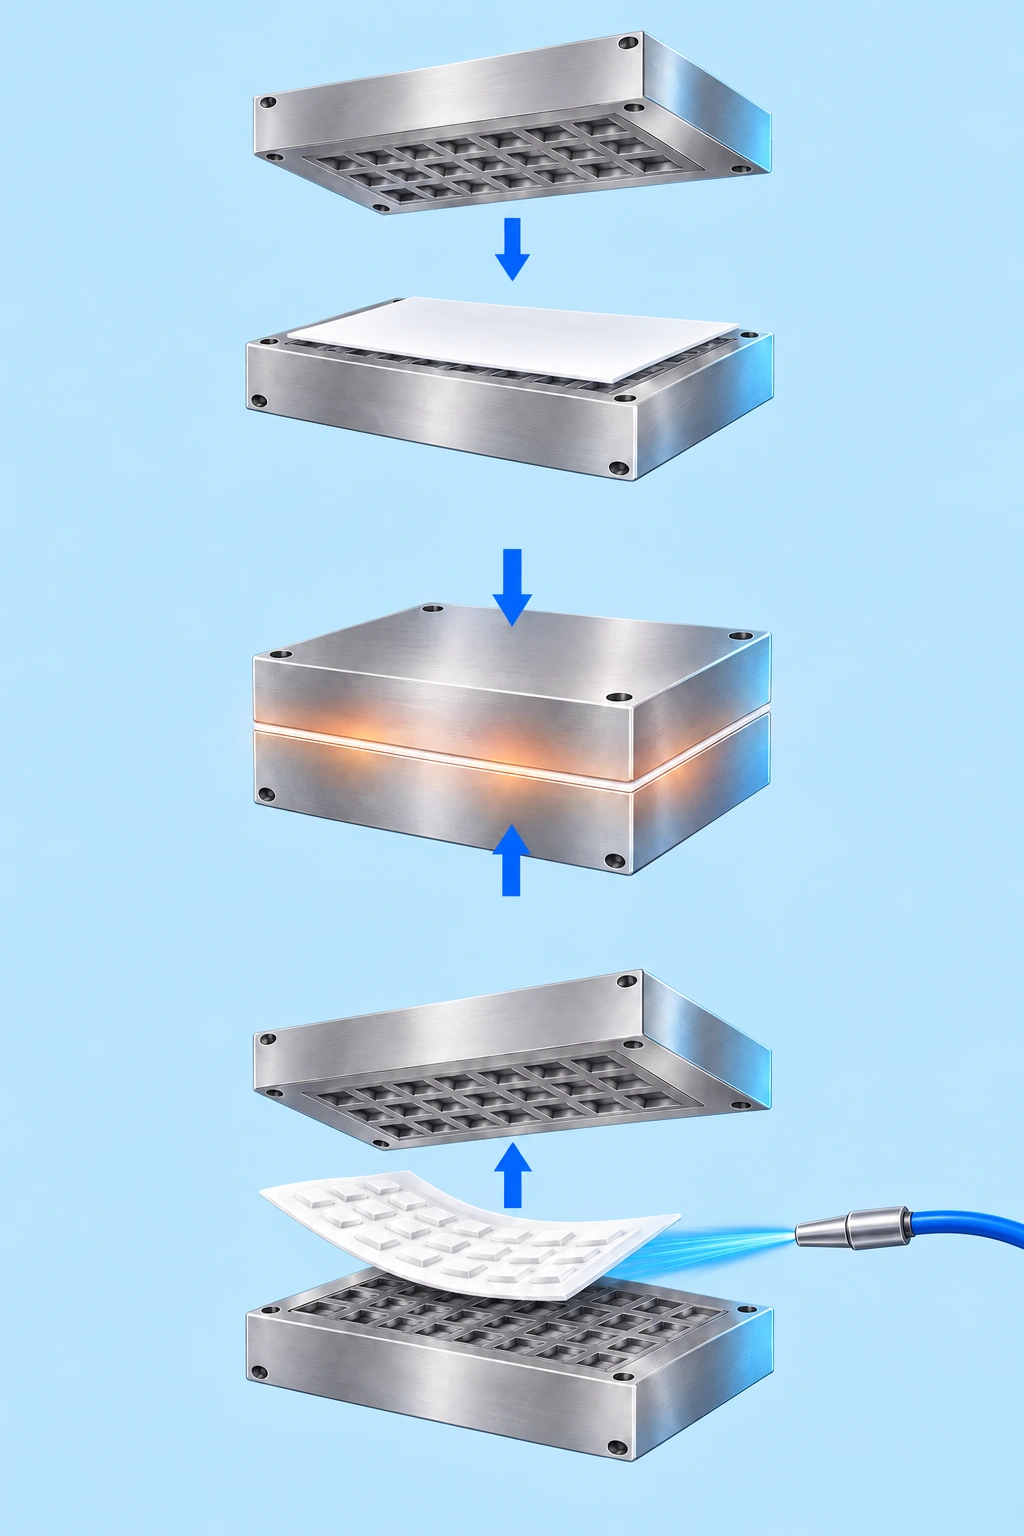
Inspect, place, cure, release and condition. Follow the five steps of the cleaning process.
POWERCLEAN / CleanPOWERWAX / ConditionPRODUCTION
- 01
Inspect
Check mold surface — clean when brightness fades or brown stains appear
- 02
Place
Place one sheet on the lower die; clearance 1.0–1.5 mm; no lead frame
- 03
Cure
Close mold at recommended pressure; wait 3–7 min until sheet cures
- 04
De-mold
Remove cured sheet completely with dry compressed air
- 05
Condition
Repeat if needed, then apply POWERWAX 1–2 shots and resume production
Before you begin
- Use in a well-ventilated place or system
- Wear heat-resistant gloves · avoid contact with hot cured sheets
- Do not directly inhale vapor released when the mold opens
- Store in a cool, dry place
06 / LET’S TALK
Let’s prepare
your next process.
From product selection to samples and custom sizes, tell us about your mold and process conditions.
hanschem1@naver.com